2026 How to Choose a Pneumatic Conveyor for Your Business?
Choosing a Pneumatic Conveyor is a practical decision about how your materials will move every day. The right system can carry powders or granules through enclosed pipes, reduce manual handling, and fit around existing equipment. The wrong one may struggle with fragile products, long routes, or frequent changes in production.
Start with the material, not the machine. Note its particle size, bulk density, moisture, temperature, and tendency to break or form dust. Then estimate the required throughput and map the route, including bends, vertical lifts, and delivery points. A short transfer across a clean factory floor has different demands from a long line feeding several silos. Small details matter.
Compare dilute-phase and dense-phase conveying against those needs. Air velocity, pipe diameter, pressure, filtration, and receiver design all affect performance. Ask suppliers how their recommendations were calculated and what material data they used. Request references or a test using your actual product, where feasible. A catalogue rating alone is not proof of reliable output.
Consider energy use, noise, cleaning access, wear parts, and operator training alongside purchase price. Check that dust collection and system safeguards suit the material and site; qualified engineers should assess the installation. Keep maintenance realistic. A system that is efficient on paper may be awkward to inspect when a filter sits behind a crowded platform. That is easy to overlook. I would not treat any preliminary estimate as a guarantee, either. Verify assumptions with measured production data and a supplier who can explain the trade-offs plainly. This guide explores the questions that help businesses choose with greater confidence, without pretending one design fits every plant.
Define Your Material and Production Requirements
Start with the material. Record its particle size, bulk density, moisture level, and temperature. These details affect how easily it moves through a pipeline. Fine powder may form dust or cling to surfaces, while damp material can build up inside bends. Fragile pellets may break if conveying speed is too high. Measure it. A small sample can reveal problems that a product sheet misses. Check whether the material is abrasive, sticky, or prone to separating during transport. These properties help determine whether dilute-phase or denser, slower conveying deserves investigation.
Next, define the production target in practical terms. Estimate the required throughput per hour, daily operating time, and distance between pickup and discharge points. Include vertical lifts, pipeline bends, and the number of destinations. A system that handles a brief peak may not suit continuous production. Feed rate matters, too: irregular loading can create surges, even when the average rate looks acceptable. Note available floor space, power, compressed air, and dust-control needs. Then compare these requirements with test results using representative material. Be cautious with estimates. Real material can behave differently after storage, and one test may not capture every shift condition. Record what remains uncertain before selecting equipment.
Set Conveying Capacity, Distance, and Layout
Before comparing pneumatic conveyor systems, define the material and the required rate. Record bulk density, particle size, moisture, and whether the product breaks easily. Estimate both average demand and the busiest production period. A powder feeding steadily may behave differently from pellets discharged in short batches. Peak matters. Build in a realistic margin, but avoid sizing only for an unlikely maximum.
Map the route from pickup point to receiving vessel. Note horizontal distance, vertical lifts, pipe diameter changes, and every bend. A compact route is not automatically an easy one; tight bends can increase wear or damage fragile particles. Allow space for filters, inspection doors, and routine cleaning. Check whether the conveying line crosses walkways or blocks access to equipment. Small layout details matter.
Match the conveying method and operating pressure to the material, rate, and route. Longer runs and more bends may require greater airflow, which can affect energy use and product quality. Include the receiver, air source, controls, and dust collection when reviewing capacity; the pipe alone does not define system performance. Ask suppliers to state their assumptions about feed rate and material condition. A pilot test can expose issues that calculations miss. A spreadsheet can make the choice look settled; it rarely is.
2026 How to Choose a Pneumatic Conveyor for Your Business?
Set conveying capacity, distance, and layout
These are illustrative planning scenarios, not guaranteed system performance: actual capacity depends on material properties, pipe diameter, conveying mode, bends, and operating conditions. Confirm the design with a qualified supplier using your material and route layout.
Compare Dilute-Phase and Dense-Phase Systems
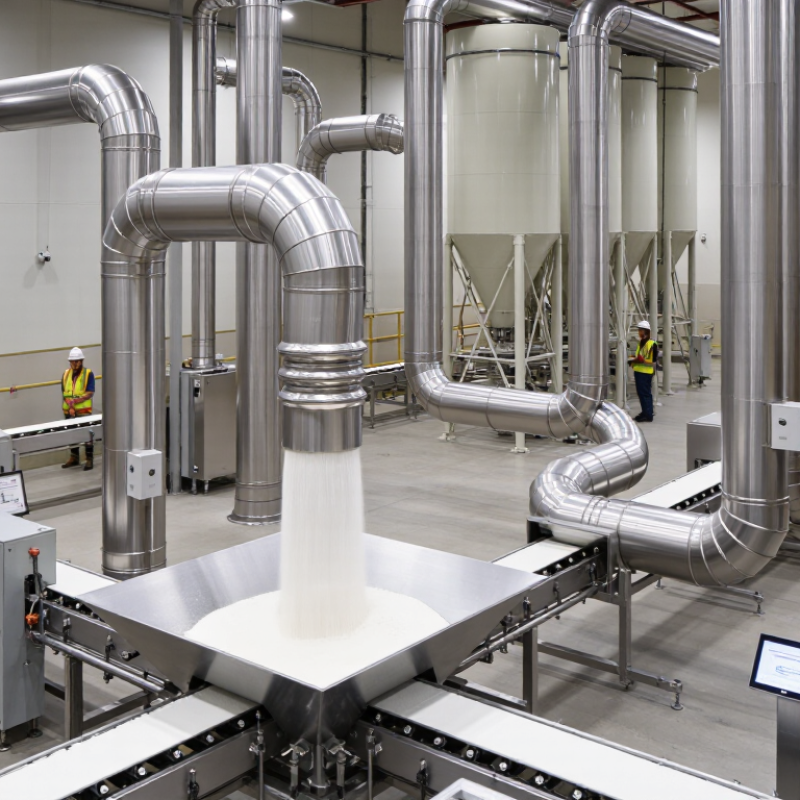
Dilute-phase conveying suspends powder in fast-moving air, often through a 75-millimeter pipe with visible bends and long routes. It suits many free-flowing materials and offers straightforward layout changes. But higher air speeds can increase pipe wear and damage fragile particles. Dense-phase systems move material in slower, heavier plugs. They can reduce particle impact and abrasion, but need closer control of pressure, feed rate, and material behavior. There is no universal winner.
Energy deserves a hard look. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that compressed air uses about 10% of industrial electricity, reaching 30% in some facilities. That figure covers compressed air broadly, not a direct comparison between conveying phases. Still, it makes leakage, air demand, and operating hours worth measuring before selecting equipment. A dense-phase system may use less conveying air in some applications, yet poor tuning can erase the advantage. I would test the actual material; brochures cannot predict every powder’s flow.
Tips: Record throughput, distance, bends, and particle sensitivity. Ask suppliers to run a conveying trial with your material, then compare energy use and wear. Small test batches can reveal awkward flow problems early.
Select System Components and Control Features
Choosing components starts with the material, not the equipment list. Check particle size, moisture, bulk density, and whether the product breaks easily. A fine powder may need a gentler conveying speed and effective filtration. A coarse, abrasive material can wear bends and pipe walls faster. These details shape the choice between dilute-phase and dense-phase conveying, as well as the blower, feeder, receiver, and pipeline diameter. Measure the actual route, including vertical lifts and tight bends. A neat floor plan can hide awkward access points.
Control features should match the process, not just the control panel. Pressure or vacuum sensors can reveal blockages and leaks before they stop production. Airflow monitoring helps maintain stable conveying, while receiver-level sensors can prevent overfilling. For systems with several destinations, automated diverter valves need clear position feedback. Operators also benefit from alarms that identify a specific fault, rather than a vague warning. Keep routine adjustments simple. Complicated settings may look capable, but they can slow a shift change.
Ask suppliers for operating data under conditions close to yours, then compare energy use, throughput, and filter-cleaning needs. Verify that controls can connect with existing plant systems, if required. A short material trial is useful. It may still miss seasonal moisture changes, so leave room for adjustment after installation. Before approval, confirm that filters and inspection points are reachable without moving nearby equipment.
Evaluate Installation, Maintenance, and Operating Costs
A pneumatic conveyor may suit a plant with limited floor space, but its installation cost depends heavily on the route. Before comparing quotes, measure the distance, vertical lift, and number of bends. Check whether the line must pass around beams, doors, or existing equipment. Small details matter. Ask the installer to inspect the actual site, not just a layout drawing. Extra supports, electrical connections, or structural changes can raise the initial bill.
Maintenance costs depend on material, duty cycle, and access. Fine powders can load filters quickly, while abrasive particles may wear elbows and pipe sections. Ask how often filters, seals, and wear parts need inspection or replacement. Keep a record of service hours and downtime from similar equipment. Estimates can miss awkward access. That happens. A filter mounted above a production line may take longer to clean than one beside a service platform.
Operating costs include electricity, labor, and production losses during stoppages. Compare expected air consumption at your required throughput, rather than relying on a motor rating alone. Include the cost of cleaning and any product left in the line after conveying. If material flow varies by season or shift, test the design against both peak and typical demand. I would not treat a precise-looking estimate as certainty; assumptions about bends, moisture, or operator practices can still be wrong. Ask for those assumptions in writing.